

Robotic welding · A closer look
See the sequence behind each resistance spot weld.
Explore resistance spot welding with part and weld identity, electrode history, repeated attempts, process records and the evidence behind quality decisions.
The practical question
How can operational information help a resistance spot-welding team?
It can help relate an identified spot-weld operation to the assembly, schedule, gun, recorded attempt and relevant electrode work. Linking that record to the appropriate inspection allows the team to investigate a specific concern without assuming that a completed squeeze-and-weld sequence establishes joint acceptance.
A body assembly can contain many recorded spot-welding operations. The review becomes useful when a particular weld, its equipment context and the associated inspection can be found together. Counting operations is a starting point; understanding what those counts represent is the next step.
Recognise the resistance-welding process
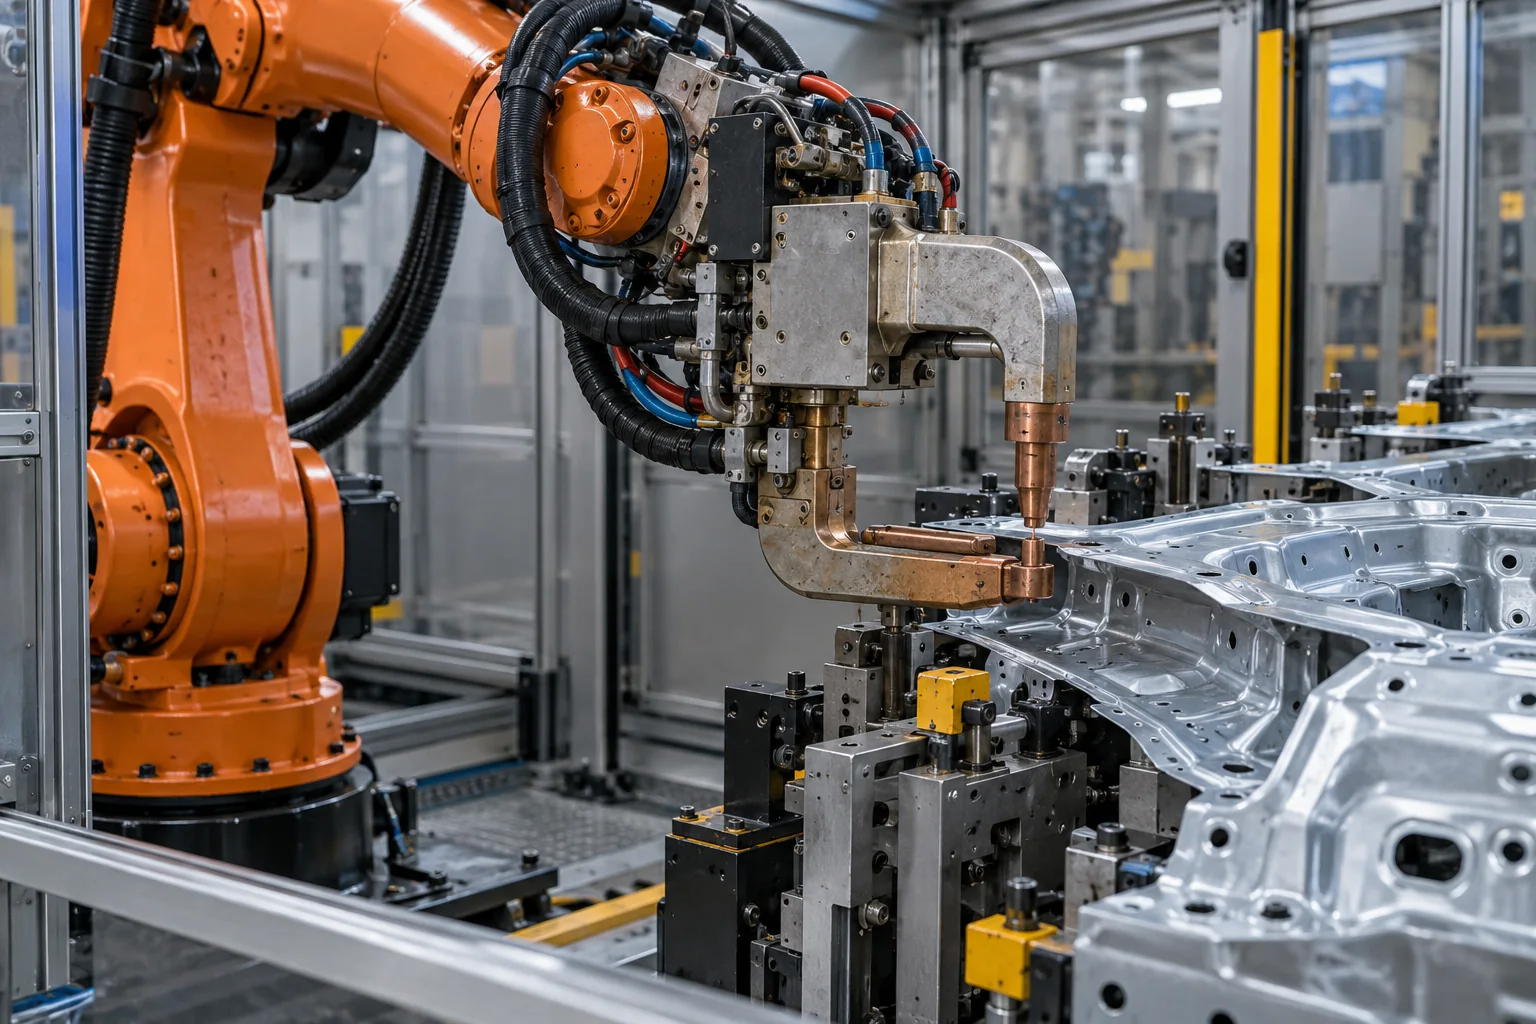
Resistance spot welding (RSW) joins sheets using force and heat generated by electrical current through the work. Electrodes contact the material, and a local weld nugget forms at the joint. This differs from an arc-welding operation, so a spot-welding record needs its own process definitions and interpretation.
Sources: [1]
Identify the gun and electrode history
TWI notes that electrode properties and selection matter to resistance spot welding. Keep the responsible gun and electrode references connected to the operation, along with recorded dressing, replacement or other work. The purpose is to make the relevant history available for review, not to diagnose a weld from an electrode counter alone.
Sources: [2]
Make weld counts understandable
Ask how the factory distinguishes a commanded weld, a completed sequence, a repeated attempt and an accepted joint. Those events answer different questions. A count that mixes them can appear consistent while leaving uncertainty about which locations received the required work.
Where the records permit, use a stable weld-location reference within the assembly. Retain the programme and schedule revision and show whether a result belongs to an original operation or a later repair. If inspection is sampled, identify the sample and its coverage explicitly. A sampled finding should not silently become an individual examination of every joint in the period.
An illustrative situation
Bring inspection back to the relevant operation
Hypothetical example: a finding on one assembly sends the team back to a production period containing several product variants. They identify the weld location, the applicable variant and the actual operation sequence before examining trends. The electrode-service entry is nearby in time, but its relationship to the finding remains a question.
The reviewer can now separate possible explanations: a record mismatch, a repeated operation, a relevant equipment change or something requiring further examination. The site’s quality and welding specialists determine the follow-up. The operational view earns its place by shortening the search for the right evidence.
Choose an evaluation people can inspect
Begin with one assembly family and a concern that repeatedly brings production, maintenance and quality together. Agree which weld identifiers and history are available today. Then walk through a few known records with the people who created or used them, noting every point where interpretation depends on memory.
A useful outcome could be a clearer account of repeated attempts, a dependable route from inspection to production context, or a better handover of open questions. Keep the review’s limits visible. VIEOX can begin the conversation around that specific information problem and the people who need a clearer answer.
Put the question to work
A practical checklist
- Define the assembly and weld-location references used in the review.
- Distinguish commanded operations, completions and repeated attempts.
- Keep the relevant gun, schedule and electrode-service history available.
- State which welds or samples an inspection result actually covers.
- Document the assessment and the next responsible person.
Questions, answered
Is an electrode-life counter a quality result?
A counter describes recorded use under its stated definition. It can help locate a maintenance or process question, but joint acceptance needs the applicable inspection and process evidence. Preserve the distinction when presenting the information to production or quality.
What if weld-location identifiers are missing?
Start by documenting the level of identity that is available, such as the assembly, programme and recorded sequence. Decide whether a more precise link can be established with the responsible team. Do not make the interface imply weld-level traceability before that connection exists.